Tube Extruder
Single Screw Extruders
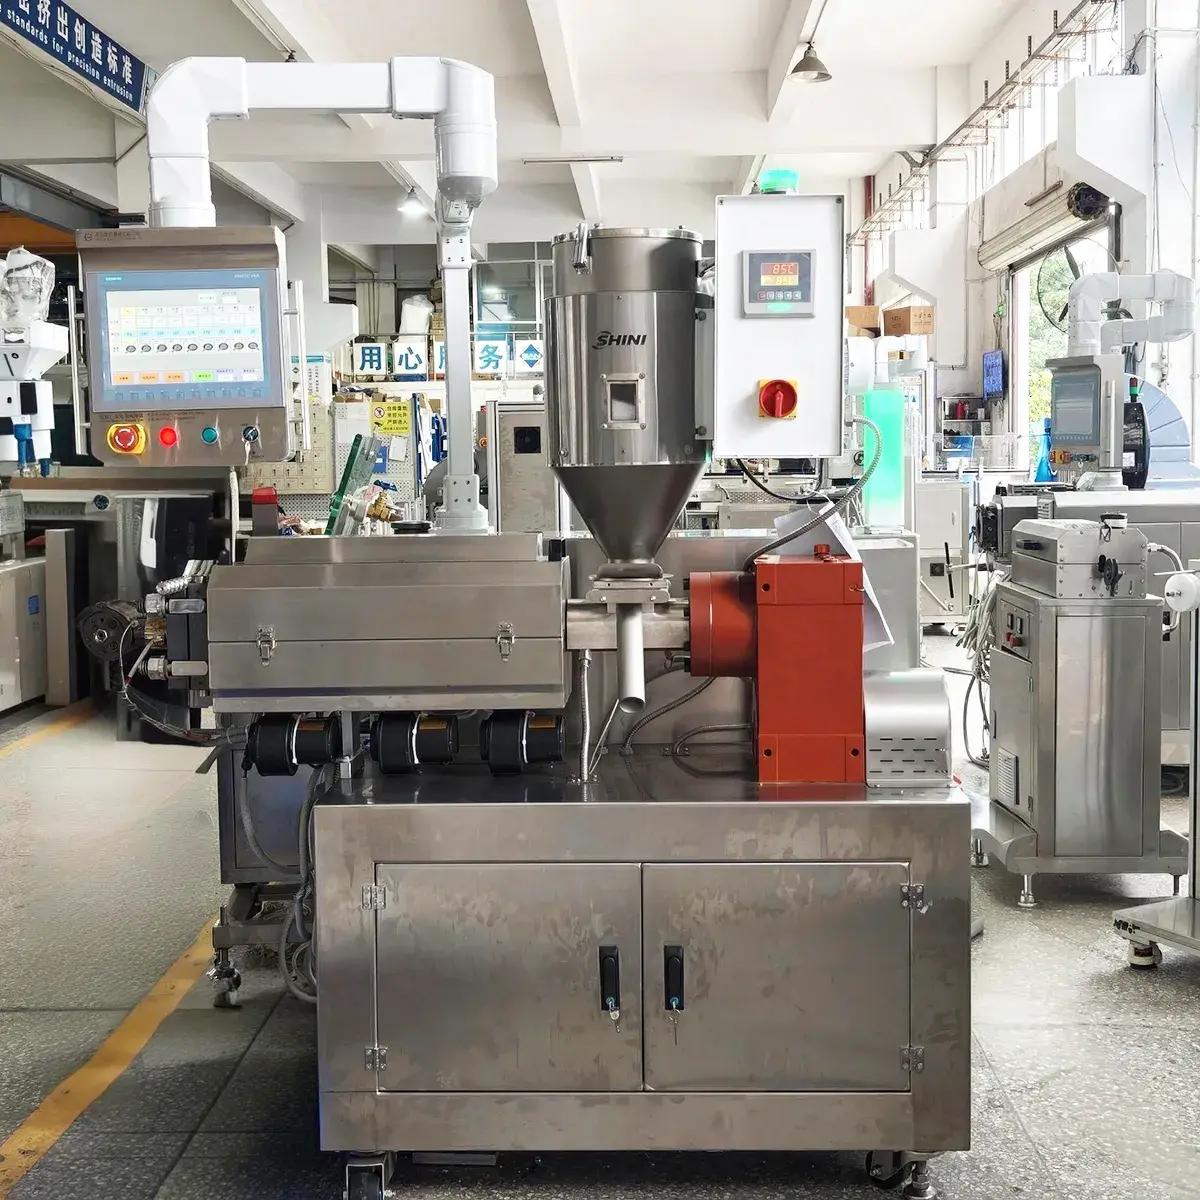
Precision tube single-screw extruders turn plastic pellets into continuous tubing. The pellets enter the barrel through a hopper, where the extrusion process begins. The motor drives the screw through a gearbox, which regulates its speed as the screw moves the material steadily through the heated barrel. The screw compresses and mixes the plastic before pushing it through a tube die, where the tubing takes its initial shape. Once formed, the tubing moves into a sizing and cooling tank, where the cooling water helps it keep the correct dimensions and shape. The haul-off unit then pulls the tubing forward at a steady speed, and the cutting unit cuts it to the required length.
Materials Processed
PVC, TPU, PE, PP, PA, and other thermoplastics
Request a Quote
Watch Videos
Applications
- Medical tubing
- Automotive tubing
- Dip tubes for shampoo, lotion, perfume, and other personal care packaging
- Precision tubing for consumer products
Technical Specifications
- Screw L/D Ratio: 25:1–33:1, with 28:1 as the standard ratio for processing medical-grade and engineering polymers
- Approx. Extruder Dimensions (L × W × H): 1800 × 1000 × 1450 mm; final dimensions depend on the screw size and extruder configuration
- Capacity (kg/h): Depends on the tubing diameter, material, and extruder configuration
Finished Product Samples
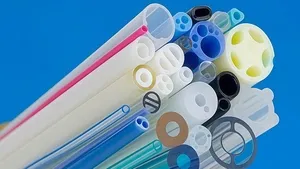 Multi-Lumen Tubing
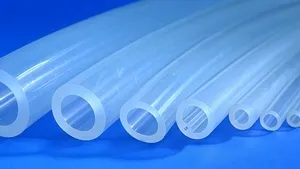 Silicone Tubing
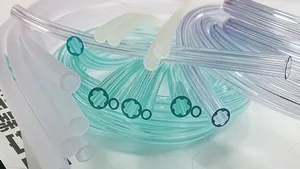 PVC Endotracheal Tubes
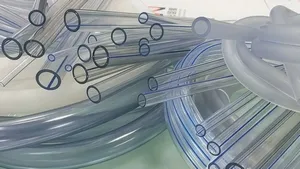 Color-Striped PVC Tubing
Features
- These single-screw extruders use a servo motor and belt drive with a two-stage transmission, which provides the torque needed for steady operation at low screw speeds.
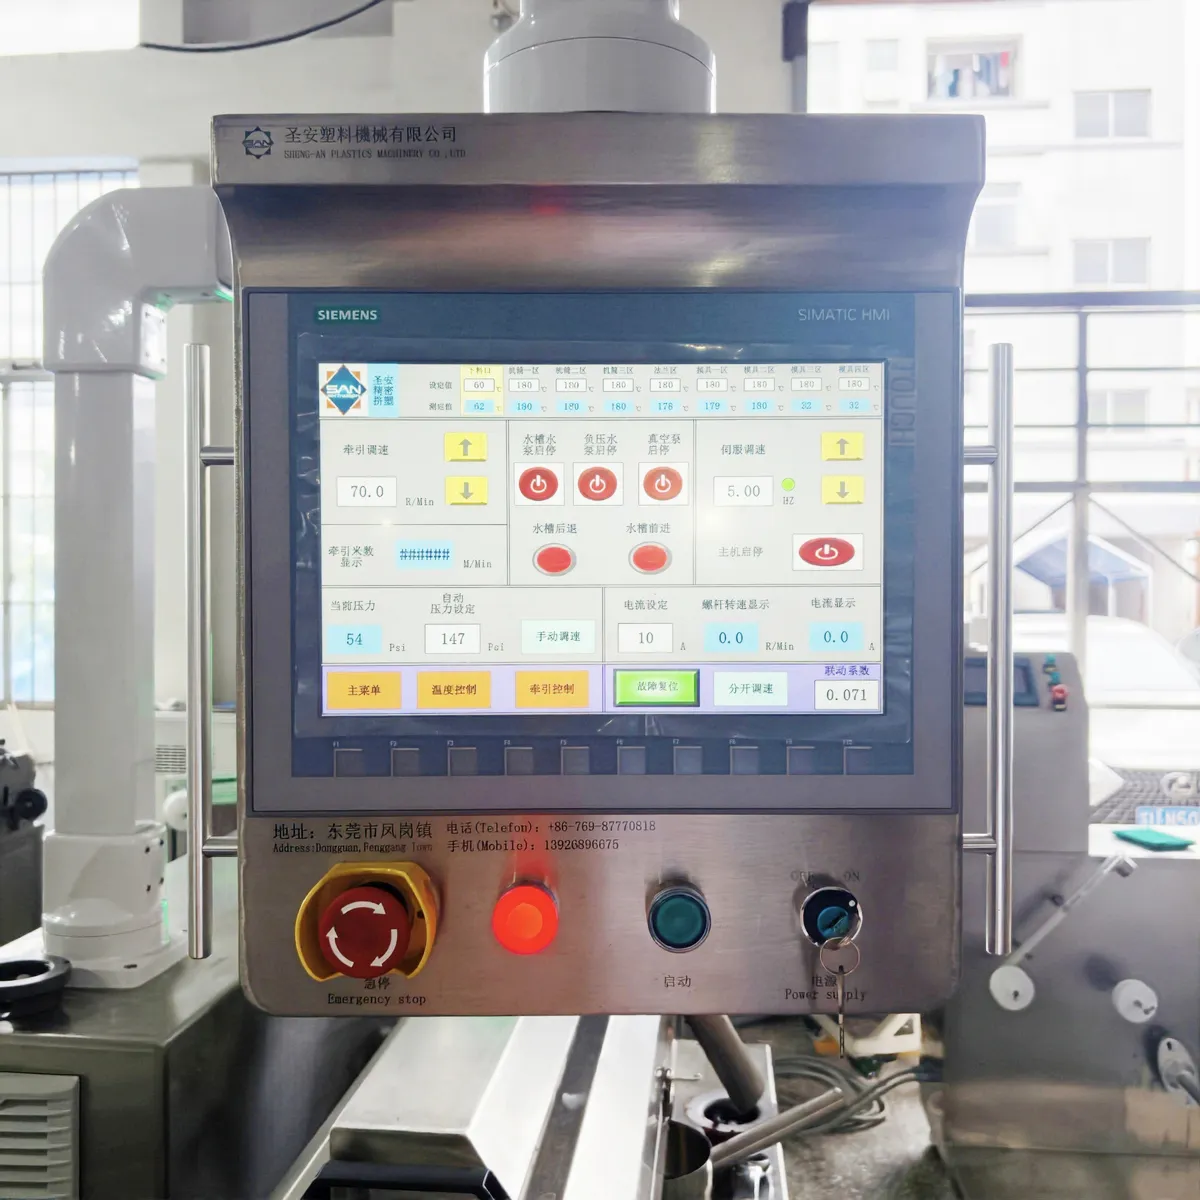
- RKC temperature controllers regulate each barrel heating zone separately and helps maintain stable temperatures throughout the extrusion process.
- Closed-loop pressure control continuously corrects changes in extrusion pressure to keep the material flow steady, even when processing at high temperatures.
- Three access levels in the Siemens PLC prevent unauthorized users from operating the extruder or changing production data. The control program also monitors overload, high and low temperatures, and abnormal extrusion pressure.
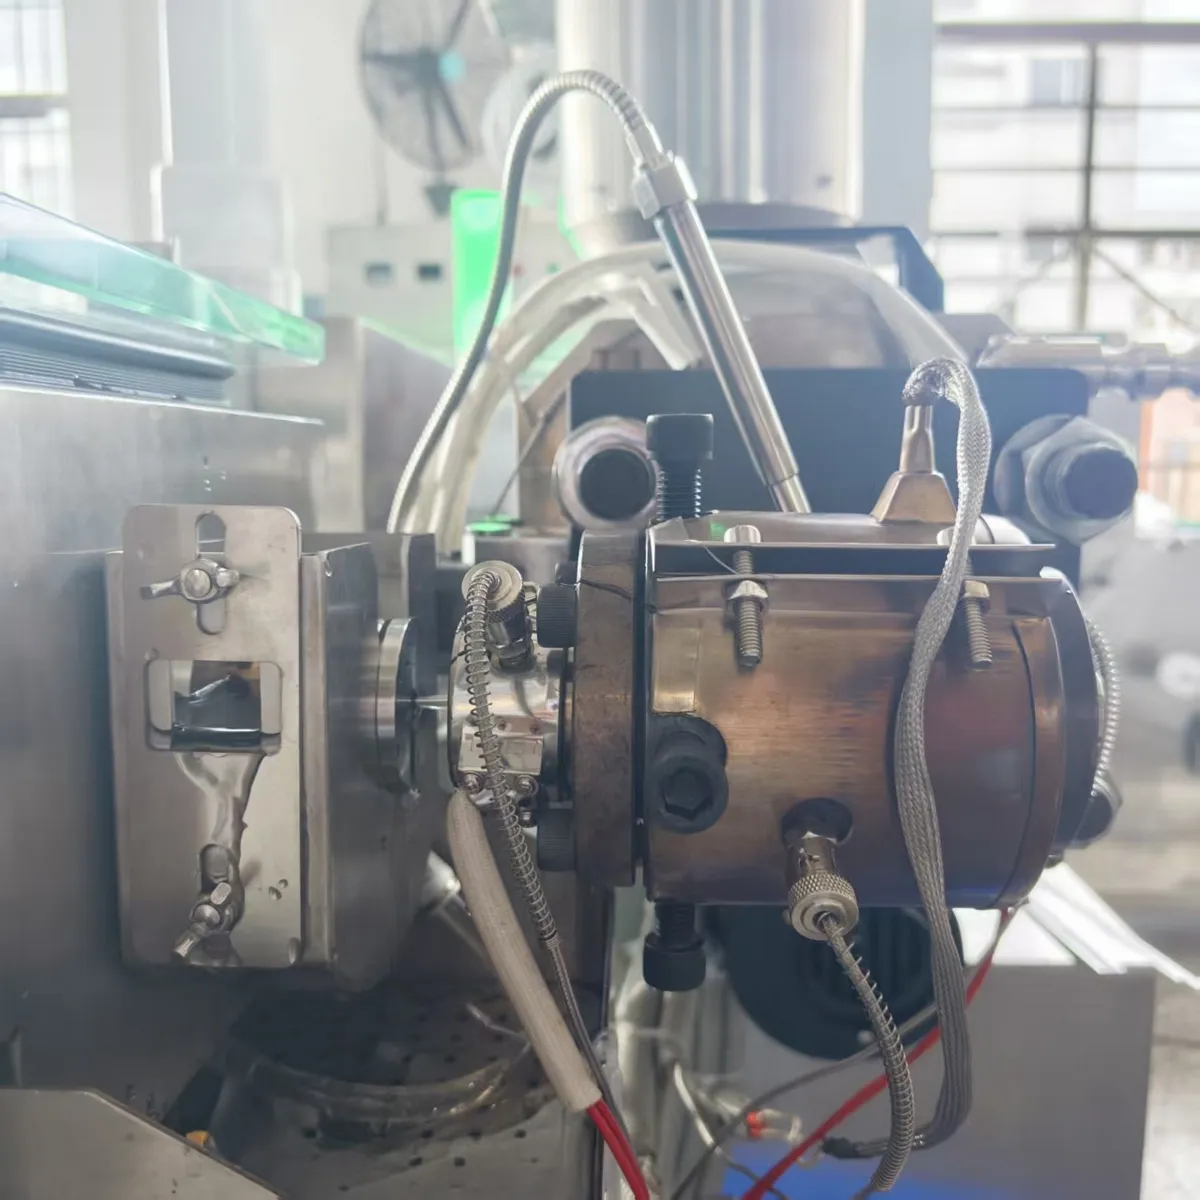
- The extrusion die includes air cooling to reduce the temperature of the material at the outlet.